
A Compression Molder Provides Large-Part Compression Molding
and Deep Draw Solutions
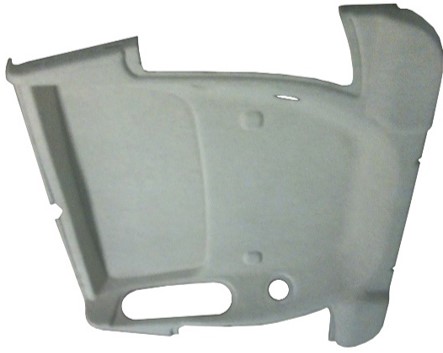
AdvancTEK’s compression molding process produces components like headliners, acoustic panels, custom trim panels, bunk trays, and wheel well liners.
💡
Key Takeaway
Layers of materials, typically a substrate and topgood, are heated and compressed to produce the final compression molded part. This process is very tunable and our experts can provide recommended material composition based on the goals of the customer such as acoustic and thermal performance, cleanability, and cost. Compression molding also suits large flat components such as data center enclosures and panels, producing thermal and acoustic panels at lower tooling cost than injection molding.
Our compression molding capabilities allow us to create elements through large-part compression molding with extremely deep draws. We can successfully create these parts in markets like commercial vehicle, construction, agriculture, and powersports.
As one of the few compression molding manufacturers in North America with large-part and deep-draw capability, AdvancTEK helps customers bring complex, large-format parts to production.
Tell Us About Your Project
Share a few details about your project, and our team will follow up with next steps.
Compression Molding Solutions
Compression molding can be a great option for low-, medium-, and high-volume applications. AdvancTEK has ten formers and nine waterjet stations throughout sites in both the U.S. and Mexico, and we use a variety of topgoods including vinyl, cloth, and non-wovens, as well as three main substrate types:
- GMT – Glass mat thermoplastic; a low-pressure, thermoformable PP based composite combined with a chopped filament fiberglass
- Dry urethane – Urethane core and fiberglass mat for strength and rigidity
- PET – Needle-punched polyester fiber
Every program is a custom compression molding build, with substrate and coverstock matched to the part’s acoustic, thermal, and structural goals.
Substrate Comparison
GMT vs. Dry Urethane: Which Is Right for You?
GMT comes in lofting and non-lofting varieties, is tuneable, and has customizable densities ranging from 600 to 2,000 GSM. It has a high stiffness-to-weight ratio, making it the best option when stiffness is a priority.
Dry urethane has an excellent I-beam structure, and the urethane composite and fiberglass can be customized to achieve densities of 680–2,000 GSM. It is an excellent lower-weight option with superior acoustic and thermal performance.
Our Compression Molding Process
As an experienced compression molder, AdvancTEK works closely with the customer to understand the technical requirements of their applications and materials. Thermal, acoustic, depth of draw, coverstock selection, heat resistance, and part rigidity are all considered to allow us to develop bespoke composite construction and provide the most cost-effective compression molding solutions for our customers.
Elements of our approach include:
- Using our custom-designed, semi-automated molding equipment, we heat thermoformable composite substrate in an oven designed specifically for our composite substrate. We bring it to a softening point that allows coverstock to be bonded to the surface and lets the composite substrate be molded into its final shape. This process is often referred to as thermoforming, or large-part thermoforming for sizable parts.
- The heated composite is indexed into a temperature-controlled compression mold where, prior to closing, cloth or vinyl coverstock is introduced using automation. Once the coverstock is introduced, the mold closes and forms the part into its final shape while bonding the composite substrate and coverstock together.
- The temperature-controlled mold extracts the heat from the composite substrate and it becomes a semi-rigid component.
- As the compression molded part indexes out of the molding equipment, it is inspected and then placed into a robotic waterjet trim cell. Here, a robot equipped with a special nozzle utilizes 50,000 psi of water pressure to trim the perimeter and interior features of the part.
- Upon completion of the robotic waterjet trimming process, the trimmed compression molded parts are placed into a check fixture where operators inspect them for dimensional accuracy, trim feature presence, and correct appearance requirements.
AdvancTEK strongly suggests that manufacturers contact us any time they are considering compression molding. Like any process, there are nuances associated with part design, material selection, and part interface with adjacent components that should be considered during the design process. Our team works alongside customers to provide them with the expertise required to optimize part design while considering quality, performance, and cost objectives.
Many customers attempt to design compression molded components, and large-part compression molding, without consulting compression molding suppliers and, more often than not, it results in costly redesigns, part delays, quality issues, and excessive part cost. AdvancTEK helps you avoid the hassle and gets the job done right the first time.
The Benefits of Choosing an Experienced Compression Molding Company
- Compression molding allows manufacturers to offer styled and aesthetically pleasing components that are also lightweight, strong, and durable while providing outstanding acoustic and thermal performance.
- In comparison to other molding processes, compression molding tooling is very cost effective and has an outstanding tool life.
- We take great pride in partnering with manufacturers to co-develop large-part compression molding solutions that meet aesthetic, performance, weight, and cost requirements. As with all processes, compression molded parts and tooling have many nuances that must be considered during the design process. Our team understands these nuances better than any other supplier in North America and works alongside our customers to optimize the design, tooling, and launch process.
- AdvancTEK currently supplies compression molded components to every major commercial vehicle manufacturer in North America as well as many agriculture and construction equipment manufacturers, a testament to our quality and industry leadership.
- Our approach of providing bespoke design and material solutions to each customer’s unique requirements continues to provide them with the cost, feature, weight, and quality advantages that they require to stay a step ahead of their competition.
- Our Dublin, Virginia and Saltillo, Mexico plants provide compression molding services to diverse organizations, serving clients in an 8-hour radius of each location.
FAQs Our Compression Molders Receive
What are some good applications for compression molding?
Interior Trim
- Headliners and wall trim (automotive, commercial vehicle, bus, recreational vehicle, powersports, construction equipment, agricultural equipment, and more)
- Closeout panels (under dash, kick panels, and more)
- Trunk lining, under bunk lining, and storage cabinet or console lining
Exterior Trim
- Underhood insulation
- Fender liners or underbody panels
Miscellaneous Applications
- Office/cubicle walls
- Noise abatement panels in large open spaces prone to echo
Do compression molded panels meet FMVSS302 (flammability) requirements?
Yes, composites utilized for compression molded parts can be engineered to meet FMVSS302 requirements.
Can compression molded panels be used in exterior applications that are exposed to the elements?
Yes, hydrophobic composites are a great, lightweight alternative to conventional plastics and repel water and other elements.
What materials are the tools made out of?
- Compression molds – These are usually composed of cast aluminum that has been machined to the final shape. The cast aluminum contains water lines that are used to control the temperature of the molds during longer production runs.
- Waterjet nests – These are usually made of a composite material that allows them to be easily adapted for future part variants (holes, cutouts, and more). The nests are encapsulated by aluminum so that the vacuum system used to hold the part in position while it is being waterjet trimmed can also collect offal and overspray.
- Check fixtures – These are usually made of a composite material marked with scribe lines and tolerance bands allowing operators to inspect parts for trim accuracy and presence of optional cut features prior to shipment.
What types of coverstock can be used in conjunction with compression molding?
Woven cloth, non-woven cloth, and vinyl can all be used with compression molding. It is imperative that AdvancTEK be consulted during the coverstock selection/qualification process so that stretch and set, moldability, and performance characteristics are assessed to confirm that the coverstock’s characteristics align with the compression molding process.
Can AdvancTEK perform value-added processes for compression molded solutions?
Yes, this is very common. Components such as insulation, lamps, wiring harnesses, reinforcement brackets, fasteners, and speakers are often assembled to compression molded panels prior to shipment to our customer. We also perform kitting and line sequencing.
Contact Us for Compression Molded Parts
Optimize your operations with the help of our experienced compression molding company. Our compression molding service covers the full scope, including material selection, molding, waterjet trimming, and value-added assembly. Reach out to AdvancTEK today to discuss your application and equipment needs, and our team can get to work on viable solutions.